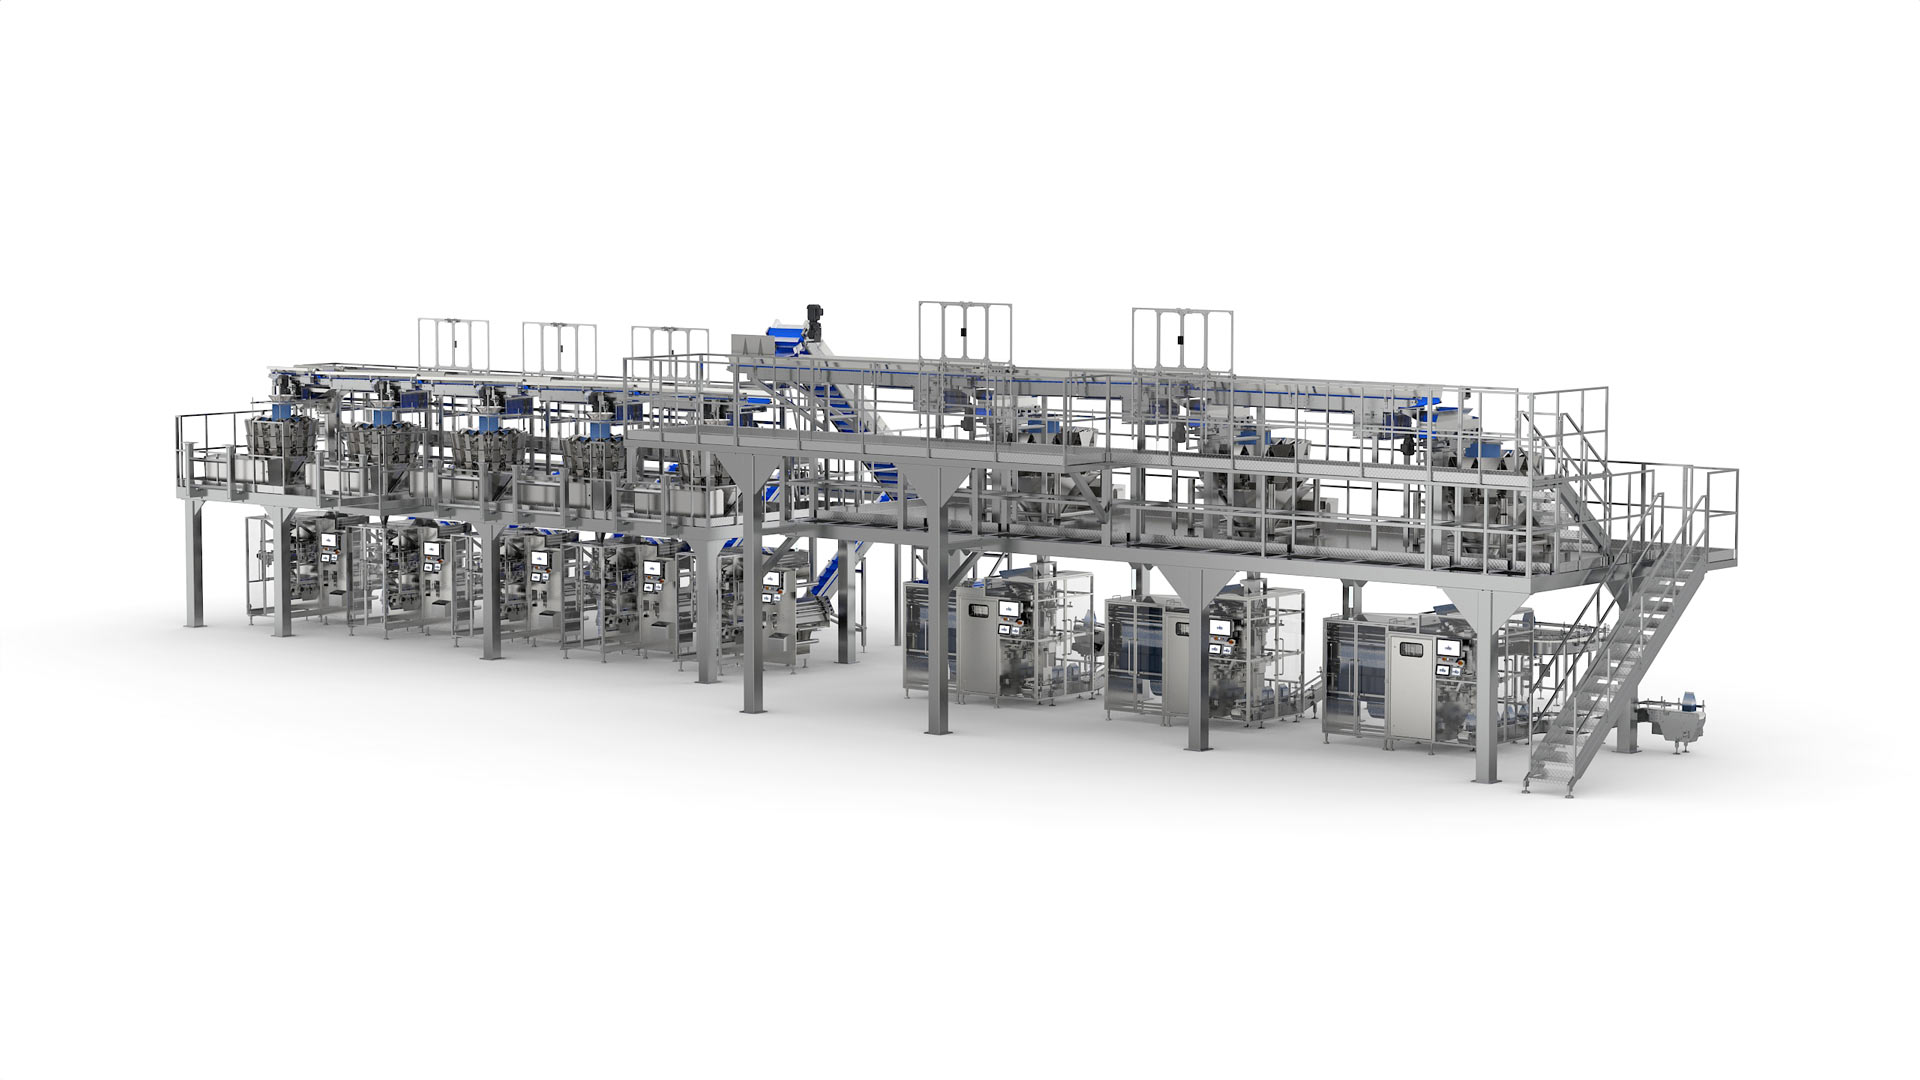
Example of a complete primary and secondary weighing and packaging line for baked savoury snacks, designed to ensure production continuity, dosing accuracy and lower operating costs.
The system integrates five RQ550 VFFS vertical packaging machines producing 30 g pillow packs and three R800 packaging machines for secondary packaging in 180 g multipack bags.
From bulk product infeed to the transfer of multipacks to the end of line, every stage is managed through integrated conveying, weighing and packaging systems.
Infeed and distribution: production adapts to operating conditions
Bulk product from the process line is conveyed on overhead vibratory conveyors and distributed to the MBP 16C3 DMA Twin primary multihead weighers.
The system automatically regulates the feed to the five primary packaging lines, distributing the product in proportion to their output capacity.
Each packaging machine runs at a nominal speed of 120 packs per minute.
If one of the five lines stops temporarily, the system redistributes the product to the remaining four, which automatically increase their speed up to 130 packs per minute each.
The customer can thus keep production running, making up part of the stopped line’s capacity without shutting down the entire plant.
Primary packaging: 30 g pillow packs with RQ550 VFFS machines
The MBP 16C3 DMA Twin multihead weighers, equipped with memory buckets and a butterfly discharge with two independent sections, dose the product for the packaging machines.
The five MBP RQ550 continuous vertical packaging machines form, fill and seal the 30 g pillow-pack bags.
The machines feature a vertical sealing system driven by brushless servomotors and digital control via touch screen.
The operator can monitor the process directly from the machine interface, which also displays a countdown of the remaining film reel time.
Automatic Reel Splicer: reel change without stopping production
The RQ550 machines integrate the Automatic Reel Splicer, which automatically splices the film from the expiring reel to the new one.
The system reduces manual intervention and maintains packaging continuity during reel changes.
A particularly important feature in a plant with five primary packaging machines, where every stoppage can affect overall output.
Automatic transfer of packs to secondary packaging
Once formed and sealed, the 30 g pillow packs are transferred by an integrated system of belt conveyors and elevators.
The packs reach the secondary packaging section, where they are grouped to produce the multipacks.
Automatic transfer connects the five primary lines to the three secondary lines, keeping the pack flow within the same plant.
Secondary packaging: 180 g multipacks with R800 VFFS machines
In the secondary packaging section, the 14C2 multihead weighers/dosers count the primary packs and feed groups of bags to the three MBP R800 vertical packaging machines.
Each multipack is a 180 g block-bottom bag containing six 30 g primary packs.
These packaging machines are also equipped with automatic reel change, to minimise interruptions during secondary packaging.
The customer therefore has an integrated process that handles the forming of individual packs, their grouping and the production of multipacks.
From multipack to end of line: continuous conveying to case packing
The 180 g multipacks are transferred to a continuous spiral conveyor, which carries them to the upper level of the plant.
From there, the packs are conveyed to the downstream case packing and end-of-line area.
This configuration connects secondary packaging to the subsequent stages of the production process, maintaining an automatic pack flow.
Component protection in dusty environments
In baked snack plants, dust and residues can compromise the reliability of electrical components.
For this reason, MBP has integrated a cooling, dehumidification and pressurisation system for the electrical cabinets.
Pressurisation prevents dust ingress, while temperature and humidity control helps maintain suitable operating conditions.
The solution reduces component exposure to the plant’s ambient conditions, improving machine reliability.
The result: production continuity and maintenance costs reduced by 10%
The line combines a compact layout with intermittent-motion packaging technology, chosen to reduce footprint and simplify plant management.
Six months after start-up, the customer recorded a reduction in maintenance costs of approximately 10% per machine compared with traditional continuous-motion systems.
A tangible result that adds to the plant’s ability to manage product distribution automatically and keep production running during temporary stoppages of a line.
A complete line designed around the customer’s needs
This application shows how the integration of multihead weighing, VFFS vertical packaging and automated handling can meet specific production requirements.
Smart product distribution limits the impact of machine stoppages. Automatic reel change reduces operational interruptions. The integration of primary and secondary packaging simplifies process management.
| Feature | Configuration |
|---|---|
| Application | Baked savoury snacks |
| Primary packaging | 5 MBP RQ550 VFFS |
| Primary weighing | MBP 16C3 DMA Twin |
| Primary format | 30 g pillow pack |
| Nominal speed per primary line | 120 packs/min |
| Compensation speed per primary line | Up to 130 packs/min |
| Secondary packaging | 3 MBP R800 VFFS |
| Secondary counting and dosing | 14C2 multihead weighers |
| Secondary format | 180 g block-bottom multipack |
| Reel change | Automatic Reel Splicer on the RQ550 and automatic reel change on the R800 |
| Conveying to end of line | Continuous spiral conveyor |
| Electrical cabinet protection | Cooling, dehumidification and pressurisation |
| Result after 6 months | Approx. 10% lower maintenance costs per machine |